


О нас
Durmapress specializes in designing, manufacturing, and selling various metal processing equipment, including bending machines, shears, punches, and laser cutting machines. The company was founded in 2014, with years of experience and technology accumulation. DurmaPress has become one of the well-known brands in China's metal processing machinery industry.


Свяжитесь с нами
Последние сообщения


Категории
Следуйте за нами
Еженедельное новое видео
Оглавление
Two press brakes with the same tonnage and bed length can run very differently depending on the CNC system driving them. The controller influences how quickly jobs can be programmed, how well the machine's axes are coordinated, and how efficiently an operator moves from setup to the first good part.
This guide compares the three brands buyers weigh most often—Delem, Cybelec, and ESA—down to the model level, then gives you a practical framework for matching a controller to the parts you bend, the axes you need, and the support you can get locally. The goal is a buying decision, not another brand tour.


1. What Is a Press Brake Controller and Why Does It Matter?
A press brake controller is the CNC unit—almost always a touchscreen panel—that turns a hydraulic press brake into a repeatable bending machine. It drives the ram to depth, positions the back gauge, calculates the bend sequence, and manages angle and crowning compensation.
On the shop floor, the controller shapes three things you deal with every shift: how long setup takes, how quickly you reach a good first part, and how easily an operator can run the job. It commands the movement; the machine's mechanical and hydraulic systems execute it.
Its core responsibilities include:
- Ram (Y-axis) depth control for the programmed angle
- Back gauge positioning across axes such as X, R, Z1, and Z2
- Bend-sequence calculation and, on higher models, collision checking
- Angle correction and crowning support to counter spring-back and bed deflection
- Program and tool-library storage for repeat jobs
- Alarm and diagnostic display for faster troubleshooting
Treat controller choice as a production decision. A control that fits your work shortens changeovers and reduces rejects; one that doesn't quietly taxes every job.
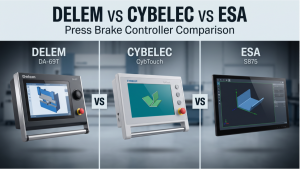
2.Delem vs Cybelec vs ESA: Quick Comparison
Each brand has a recognizable positioning, but none is universally best. Use this as a starting orientation, then confirm capability at the model level—brand-wide labels rarely apply evenly across a full product range.
| Бренд | Origin | General positioning | Typical fit |
|---|---|---|---|
| Делем | Netherlands | Broad range from conventional controls to high-end 2D/3D systems, with offline programming | High-mix work and complex parts |
| Cybelec | Switzerland | Both straightforward CNC controls and more advanced graphical solutions | Simple-to-medium bending and OEM-integrated machines |
| ESA | Italy | Practical CNC capability with graphical and DXF features on higher models | Value-focused buyers who still want modern functions |
The important detail is that all three brands now offer both simpler and more advanced controls. The right question is not "which brand," but "which model, with which capabilities, for my parts."
3.How to Choose a Press Brake Controller
Most buyers don't need a brand introduction—they need to know which control fits their work. Weigh these factors against your real workload before shortlisting anything.
- Part complexity – simple brackets and panels versus multi-bend enclosures or long structural parts
- Number of axes – Y1/Y2 plus X, R, Z1/Z2, and crowning, matched to the geometry you actually produce
- 2D vs 3D programming – whether your parts justify full 3D simulation or run fine with 2D
- CAD and offline programming – DXF import and office-to-machine job preparation for higher volumes
- Operator experience – how much guided, graphical support your team needs
- Retrofit vs new – whether you're specifying a new machine or upgrading an existing one
- Service and support – local technicians, spare parts, software updates, and parameter backup
A shop bending hundreds of identical brackets has different priorities than a job shop quoting a new part daily. Rank these for your own production first; the model choice follows from that ranking.
4.2D vs 3D Press Brake Controllers: Which One Do You Need?
The clearest dividing line in any Листогибочный пресс с ЧПУ control range is 2D versus 3D programming, and it drives both price and complexity.
2D controllers let the operator enter each bend by length and angle, usually with a cross-section view. They handle the bulk of everyday work—brackets, panels, boxes, and standard sheet metal. 3D controllers let you draw or import the full part, then automatically calculate the bend sequence and check for collisions between the part, tooling, and machine before the first stroke.
In general, 2D controls have a shorter learning curve than advanced 3D systems, while 3D adds cost and setup depth in exchange for simulation that protects tooling on complex jobs. This table shows where each typically earns its place:
| Требование | 2D | 3D |
|---|---|---|
| Simple brackets | ✓ | |
| Repeat jobs | ✓ | |
| Multi-bend parts | ✓ | ✓ |
| Collision checking | Basic / model dependent | ✓ |
| CAD / DXF import | Model / software dependent | ✓ |
| Offline programming | Model / software dependent | ✓ |
| High-mix production | Possible | ✓ |
| Full 3D visualization | ✓ |
The takeaway: 3D pays back when parts are complex, sequences are collision-prone, or job mix is high. If most of your work is simple and repeatable, a capable 2D control usually delivers a better fit for the money.
5. Delem Press Brake Controllers
Delem is one of the most established press brake control brands, with a range that runs from conventional controls to high-end 2D and 3D graphical systems. Its offline software—Profile-T and Profile-S—supports office programming with 2D/3D part building, bend-sequence calculation, and collision detection, which keeps the machine bending instead of waiting on programming.
5.1 Delem DA-53T vs DA-66T vs DA-69T
The practical decision inside the Delem range is where you land between straightforward 2D control and full 3D. The values below are typical/reference points—confirm exact capability on the official model page for the configuration you're quoting.
| Контроллер | Programming | 3D Programming | Автономное программное обеспечение | Typical Use |
|---|---|---|---|---|
| Delem DA-53T | 2D graphical / numerical | Нет | Package dependent | Standard 2D bending, fewer axes |
| Delem DA-58T | 2D graphical | Нет | Да | Faster setups on more varied 2D parts |
| Delem DA-66T / DA-66S | 2D graphical | No full 3D programming | Да | Higher-productivity 2D work |
| Delem DA-69T / DA-69S | 2D + 3D graphical | Да | Profile-T3D / Profile-S | Complex, high-mix, and tandem work |
Delem officially defines the DA-66T as a 2D graphical front-end and the DA-69T as a 3D graphical front-end. Note that "no full 3D programming" on the DA-66T does not mean no 3D capability at all—its feature set still includes automatic bend-sequence calculation, collision detection, and full 3D machine set-up. The practical decision is whether you need full 3D part programming and visualization (DA-69 class) or a strong 2D graphical workflow (DA-66 class) is enough.
6.Cybelec Press Brake Controllers
Cybelec offers both straightforward CNC controls and more advanced graphical solutions, so the exact model matters more than a single brand label. The CybTouch line is known for clean, icon-based operation, while higher or specialized platforms cover more demanding multi-axis and OEM-integrated machines.
6.1 Cybelec CybTouch Controllers
The CybTouch range spans quick single-bend work up to graphical programming that moves from sampling into production. Capability varies by model, so match the unit to your part mix rather than assuming the whole family behaves the same.
- CybTouch 8 – economical, icon-based control with an "EasyBend" page for quick single bends and automatic calculation of angle, pressure, and depth
- CybTouch 12 – mid-range unit for drawing parts on screen with automatic bend-sequence calculation, suited to moving from samples to batches
- CybTouch 15 – higher-end, glove-compatible control with larger program capacity, internal backup, and remote diagnostics
Cybelec is often a strong fit when operation needs to stay direct and efficient at the machine, and when your team or maintenance staff already know the environment. For more advanced 3D programming and offline simulation, Cybelec also offers VisiTouch and VisiTouch MX solutions. For advanced multi-axis or tandem machines, confirm the specific platform and OEM integration rather than relying on the CybTouch positioning alone.
7. ESA Press Brake Controllers
ESA Automation covers standard-to-premium CNC bending across its S-series, with the exact feature set depending on the model. Entry and mid-range units provide ergonomic operation and multi-axis support; higher-end systems add larger multi-touch screens, DXF import, tool and die library management, 3D visualization, and Industry 4.0 connectivity.
7.1 ESA S-Series Controllers
The practical split within ESA mirrors the wider 2D/3D decision, with pricing that tends to sit competitively against comparable models from other brands.
- ESA S630 / S640 – 2D controllers for standard bending, with ergonomic HMI, integrated PLC, and multi-axis support
- ESA S875 – flagship unit with a large frameless multi-touch screen, DXF file support, advanced tool/die library management, 3D bend visualization, and a standard Industry 4.0 interface
ESA is worth a close look when you want modern CNC functions—including DXF import and 3D—without automatically defaulting to the highest-cost option in the room. As with any brand, the supplier's integration and local support carry real weight.
8. Model-Level Comparison at a Glance
Buyers increasingly search at the model level, not just the brand level. This cross-brand snapshot groups comparable controls by capability so you can compare across brands directly. Treat the entries as typical/reference positioning and verify against current official model pages before purchase.
| Контроллер | Programming | 3D | Offline | Typical positioning | Key consideration |
|---|---|---|---|---|---|
| Delem DA-53T | 2D | Нет | Model / package dependent | Standard CNC bending | Entry-level |
| Delem DA-66T | 2D | No full 3D | Package dependent | Higher-productivity 2D | Includes 3D machine set-up |
| Delem DA-69T / DA-69S | 2D / 3D | Да | Profile-T3D / Profile-S | Complex, high-mix, tandem | Full 3D programming |
| Cybelec CybTouch 8 / 12 / 15 | Model dependent | Model dependent | Model dependent | Entry to mid-range | Exact model matters |
| Cybelec VisiTouch / VisiTouch MX | 2D / 3D graphical | Да | Model dependent | Advanced graphical work | 3D and offline path |
| ESA S630 / S640 | 2D | Нет | Model dependent | Standard bending, value | OEM configuration |
| ESA S875 | 2D / 3D | Да | Model dependent | Advanced applications | DXF / 3D |
9.Controller Selection by Application Scenario
Feature lists don't bend metal—applications do. These scenarios turn the decision framework into concrete guidance you can map to your own floor.
| Приложение | Prioritize | Practical guidance |
|---|---|---|
| Simple brackets, panels, repeat parts | Easy 2D programming, fast setup | A capable 2D control usually gives the best fit |
| Job shop, frequent part changes | Graphical programming, auto sequencing, tool library, offline | Favor a mid-to-high graphical control |
| Complex enclosures, multi-bend parts | 3D visualization, collision detection | 3D reduces trial-and-error and protects tooling |
| Long workpieces or tandem press brakes | Multi-axis synchronization, controller-machine integration | OEM engineering matters as much as the brand |
| Retrofit projects | Compatibility, parameter backup, drive/axis condition | Confirm feasibility before committing |
Tandem bending deserves a specific note. A tandem press brake couples two machines to bend extra-long parts as one coordinated system, controlling multiple Y axes across both frames. Controller choice there depends on synchronization and integration—not screen size or axis count alone.
9.1 Example: Choosing a Controller for Three Typical Shops
The clearest way to see the framework in action is to map it to real shop profiles:
Shop A — Simple repeat brackets. A 4-axis machine, straightforward bends, steady repeat production, no CAD workflow. The priority is easy 2D operation and reliable back gauge positioning. A mid-range 2D graphical control covers this well without paying for 3D features that won't be used.
Shop B — High-mix enclosure production. Many drawings, 6–8 axes, frequent changeovers, and a CAD-driven workflow. Here 3D visualization, collision detection, and offline programming can reduce setup time and trial-and-error on complex jobs. A 3D-capable control such as a Delem DA-69-class or ESA S875-class unit fits the work.
Shop C — Retrofit of an older press brake. A mechanically sound hydraulic machine with existing linear scales and back gauge. The priority shifts to compatibility: drive and axis condition, feedback systems, and parameter backup. The best controller here is the one a technician confirms will integrate cleanly with the existing hardware.
10.New Machine, Retrofit, or Replacement?
When an older press brake struggles, the controller is often blamed first—sometimes correctly, sometimes not. Work through the decision in order rather than defaulting to a swap or a new machine.
- Diagnose the real problem. A fault may be a parameter, drive, encoder, wiring, sensor, or memory issue rather than a failed control.
- Consider a retrofit when the frame, hydraulics, axes, and back gauge are mechanically sound but the control is obsolete or slowing setup.
- Consider replacement when the machine is undersized, inaccurate, unsafe, leaking, or too slow for current demand.
A press brake retrofit controller upgrade on a mechanically strong machine can be a smart investment; the same spend propping up a worn frame usually is not. Weigh retrofit cost, downtime, and remaining machine life against the value of a new листогибочный станок, and have a technician confirm feasibility before committing.
11.Total Cost of Ownership: What Buyers Often Miss
Purchase price is the smallest part of what a controller costs to own. The real economics show up over years of production:
- Operator training time and how fast staff become productive
- First-part setup time across your typical job mix
- Scrap reduction from accurate simulation and correction
- Offline software licenses and CAD/CAM integration
- Spare parts availability and service response time
- Downtime risk if support is slow or parts are scarce
The math cuts both ways. In high-mix production, a more capable control can justify its cost by shrinking setup and scrap. For stable, repeat work, a simpler control often wins on total cost because you never pay for features you don't run.
12.Questions to Ask Before Choosing a Press Brake Controller
Bring specifics to the supplier conversation—vague requirements lead to over- or under-buying. Have clear answers to these:
- What parts will you bend most: material, thickness, bend length, and tolerance?
- How many axes does the machine need to control?
- Do you need 2D or 3D programming for your part mix?
- Do you need offline programming or DXF/CAD import?
- Do your parts require crowning or angle correction?
- How easy is it to back up parameters and programs?
- What local service, spare parts, and training are available?
- Can the supplier test the control with your actual drawings or a sample workpiece?
That last point is the most revealing. A supplier willing to demonstrate a bend on your real part—checking accuracy, оснастка для листогибочных прессов fit, and ease of operation—is showing you something useful before any money changes hands.
13. Final Recommendation
There is no single best press brake controller, only the best fit for your parts, axes, and budget. Use each brand's range as a guide, then confirm at the model level:
- Делем – deep 2D-to-3D range, strong offline programming, and a common fit for high-mix and complex work
- Cybelec – both direct CNC controls and graphical solutions; strong when operation needs to stay simple at the machine
- ESA – modern CNC capability, including DXF and 3D on higher models, at competitive value
For tandem, retrofit, or customized machines, confirm the complete control architecture and OEM integration before deciding—that detail matters more than the badge. Share your drawings, material specs, production volume, and axis needs with your supplier, and let the recommendation follow the work rather than the spec sheet.
14.FAQ
Q1: What makes a press brake controller easy to learn?
Answer: Controllers with clear graphical interfaces, guided programming, and straightforward bend-sequence workflows generally have a shorter learning curve. Actual training time depends on the controller model, machine configuration, and operator experience.
Q2: Is a 3D press brake controller worth the extra cost?
Answer: It's worth it when you bend complex, multi-bend, or collision-prone parts, or run high-mix production where simulation cuts trial-and-error. For mostly simple, repeatable parts, a capable 2D control usually gives a better fit.
Q3: Does a press brake controller control the back gauge?
Answer: Yes. The controller positions the back gauge along axes such as X, R, and Z1/Z2, depending on the machine configuration. More axes allow more complex part positioning but require a control that supports them.
Q4: What is the difference between a 4-axis and 6-axis press brake controller?
Answer: Axis count refers to how many movements the control coordinates. A 4-axis configuration may cover Y1/Y2 plus X/R back-gauge movement, while additional axes such as R, Z1/Z2, or other auxiliary movements can provide more flexibility for complex geometries. The exact axis count and its definition depend on the machine and controller configuration.
Q5: Can a press brake controller import DXF files?
Answer: Some higher-end controllers and their offline software support DXF import, letting you build programs from CAD drawings. Availability depends on the specific model and software package, so confirm it for the unit you're considering.
Q6: Can an old press brake be upgraded with a new controller?
Answer: Often yes, if the frame, hydraulics, and axes are mechanically sound and compatible. Have a technician assess the machine first to confirm feasibility, drive and feedback condition, and cost before planning a retrofit.
Q7: Does the controller determine bending accuracy by itself?
Answer: No. The controller commands the movement, but accuracy also depends on linear scales, servo valves, frame rigidity, back gauge precision, crowning, tooling, and material variation. A premium control cannot compensate for a poorly built or worn machine.