The Complete Guide to Press Brake Tooling: Types, Materials & Selection Tips
Quick answer: Press brake tooling includes punches, dies, holders, clamping systems, and forming accessories. The main tooling types are selected according to the bend shape, material thickness, required radius, flange clearance, and machine clamping standard.
For standard bends, a straight punch and V die are commonly used. Box or tray parts often require a gooseneck punch for clearance. Acute bends, hems, large radii, and Z-bends require dedicated punch and die profiles. The tooling system must then match the machine holder, clamping method, working length, and required production changeover speed.
1. What Is Press Brake Tooling?
Press brake tooling refers to the punches, dies, holders, clamping systems, and forming accessories used on a press brake to bend sheet metal into specific angles, radii, and profiles.
A complete tooling setup normally includes two core forming tools:
Punch — the upper tool mounted on the ram. It moves downward to press the sheet metal into the die and determines the bend angle, inside radius, and clearance condition.
Die — the lower tool mounted on the worktable. Its V-opening supports the sheet during bending and directly affects required tonnage, inside bend radius, springback, and cracking risk.
In real production, press brake tooling is more than just punches and dies. A complete tooling system may also include tool holders, clamping systems, crowning compensation tools, hemming tools, radius inserts, offset tools, and adapters for different machine standards.
Need tooling for a specific machine or part? Explore our standard and custom utillaje para prensas plegadoras, including punches, V-dies, segmented tooling and specialty forming tools.
Quick Press Brake Tooling Selection Guide:
| Selection Priority | What to Check | Tooling Decision |
|---|---|---|
| Bend geometry | Standard bend, box, hem, radius, offset, or acute angle | Choose a straight, gooseneck, hemming, radius, offset, or acute punch |
| Material and thickness | Material grade, thickness, surface sensitivity, cracking risk | Select punch radius, die opening, tool material, and allowable load |
| Flange clearance | Wall height, return flange, channel or tray geometry | Check whether a gooseneck punch or special profile is required |
| Machine standard | European, American, WILA, Trumpf, or other interface | Verify tang profile, holder, clamping system, and adapter compatibility |
| Production changeover | Repetitive work, high-mix work, manual or automated setup | Choose suitable tooling length, segmentation, and clamping method |
Tooling quality directly affects bend accuracy, minimum bend radius, springback control, surface finish, tool life, and production throughput. Selecting the correct punch, die, holder, and clamping system is therefore essential for stable bending results.
Press brake tooling is only one part of the complete bending system. For a broader overview of press brake types, working principles, calculations, and selection, see our Press Brake Guide.
2. Press Brake Tooling Types
Press brake tooling can be grouped into four main categories: punch profiles, die types, holders and clamping systems, and special forming accessories.
Punches determine the bend shape, clearance and achievable angle. Dies support the material and influence the V-opening, inside radius and required bending force. Holders and clamping systems secure the tooling to the press brake, while special tooling is used for applications such as hemming, offset bends, large-radius forming and surface-sensitive parts.
The correct tooling type should be selected according to the required bend geometry, material thickness, flange clearance, machine interface and production requirements.
2.1 Press Brake Punch Types
The punch is the upper tool that makes direct contact with the sheet metal during bending. Punch selection determines the achievable bend angle, minimum flange length, and whether the punch body will interfere with already-formed features on the part. The following are the most common punch types used in industrial press brake operations.
2.1.1 Standard Straight Punch
The standard straight punch is the most widely used punch type in press brake operations. It has a straight body with a pointed or slightly radiused tip, typically available in 85°, 88°, or 90° included angles.
Tip radius options:
- 0.2 mm — for tight bend radius on thin sheet
- 0.6 mm — general purpose, most common
- 1.0 mm and above — for softer materials like aluminum to prevent surface marking
Suitable for:
- Standard 90° bends on flat sheet
- Air bending and bottoming operations
- Mild steel, stainless steel, and aluminum in standard thicknesses
Not suitable for: Parts with tall side walls where the punch body would collide with the already-formed flange.
2.1.2 Gooseneck (Swan-Neck) Punch
A gooseneck, also called a swan-neck punch, has a relieved body that provides clearance around previously formed flanges and return bends. It is used when a straight punch would collide with the workpiece during box, tray, channel, or return-flange bending.
Before selection, verify the throat depth, punch profile, target bend angle, required flange clearance, tool load rating, and machine stroke. The punch body must clear the tallest formed wall throughout the complete bending sequence.
Suitable for:
- Box and tray fabrication
- U-channel profiles
- Parts with return flanges
- Bends where a straight punch would interfere with an already formed feature
2.1.3 Acute Angle Punch
Acute angle punches have a tip angle below 60°, typically 30° or 45°. They are used when the finished bend angle is sharper than what a standard punch can achieve without bottoming into the die.
How it works: In air bending, the punch tip angle must be smaller than the target bend angle to allow springback compensation. Very acute bends may require dedicated acute-angle tooling and a verified bending sequence. Confirm punch angle, die opening, springback allowance, material ductility, and tooling load capacity before production.
Common tip angles: 30°, 45°
Suitable for:
- Acute bends below 60° on finished parts
- Locking seam profiles
- Architectural trim with sharp return angles
Note: Acute punches apply concentrated force on a very narrow contact area. Always verify that the tonnage does not exceed the tool's rated capacity per meter, especially on thicker material.
2.1.4 Hemming Punch
A hemming punch is used in a two-stage process to create a closed hem — a folded edge where the sheet is bent back flat against itself. The first stage uses suitable acute-angle tooling to pre-bend the edge. The second stage uses a dedicated hemming tool to close the fold. The exact sequence, angle, clearance, and tonnage must be verified for the material and tooling system. The second stage uses the flat face of the hemming punch to press the fold completely closed.
Two-stage process:
- Pre-bend the flange using suitable acute-angle tooling.
- Close the pre-bent flange with a dedicated hemming tool, following the tooling supplier’s tonnage and clearance limits.
Suitable for:
- Safety edges on sheet metal enclosures
- Appliance panels and door edges
- Any application requiring a smooth, rounded closed edge
2.1.5 Radius Punch
A radius punch has a curved tip profile instead of a sharp point. Rather than forming a creased bend, it produces a smooth arc across the bend zone, distributing the deformation over a larger area.
Tip radius options: Typically R3, R5, R8, R10, R15 mm — must be specified based on the target inside bend radius of the part.
Suitable for:
- Architectural and decorative sheet metal with visible rounded profiles
- Aluminum and soft materials where crease marks are unacceptable
- Parts requiring a specific inside radius for structural or aesthetic reasons
Selection rule: Select the punch radius according to the target inside radius, material properties, bending method, die opening, and available tonnage. The finished inside radius is influenced by the complete tooling and material combination, not the punch radius alone. Using a radius punch that is too large will result in a flatter arc than specified.
2.1.6 Offset / Z-Bend Tooling
Offset or Z-bend tooling uses matched tool geometry to form two opposing bends and create a stepped profile. The required geometry depends on the offset height, material thickness, bend radii, and available tonnage. It is not interchangeable with a swan-neck punch unless the complete tooling geometry has been verified for the intended part.
Suitable for:
- Z-bends and stepped profiles
- Parts requiring a controlled parallel offset
- Applications where two opposing bends are formed in one setup
Press brake punches play a key role in determining bend shape and clearance conditions. Different punch profiles are used for different forming scenarios.
Learn more about press brake punch types.
2.2 Press Brake Die Types
Press brake dies support the sheet metal during bending and determine the V-opening, contact points, formed inside radius and required bending force. Die selection should match the material thickness, bend angle, target radius, flange length, bending method and tooling load limit.
2.2.1 V Dies
V dies are the most common lower tools used in press brake bending. They have a V-shaped opening that supports the sheet while the punch forms the bend.
Common V-die configurations include single-V dies, double-V dies, four-V dies and multi-V dies. A multi-V die provides several opening widths in one tool, allowing operators to select a suitable V-opening for different material thicknesses and bend requirements.
Use V dies for standard air bending, bottoming and general sheet metal fabrication. The selected V-opening should be verified against material thickness, required inside radius, minimum flange length and available press brake tonnage.
For detailed V-opening calculations and die-size guidance, see our Press Brake V-Die Opening Chart and Selection Guide.
2.2.2 Hemming Dies
Hemming dies are used to form a folded sheet-metal edge, often called a hem. This type of tooling is commonly used when a part requires a safer edge, improved stiffness or a cleaner finished appearance.
A closed hem is normally formed in more than one stage. The edge is first pre-bent with suitable acute-angle tooling, then closed using dedicated hemming tooling. The final configuration should be checked against material thickness, bend radius, finished hem profile and tooling load capacity.
Hemming dies are commonly used for appliance panels, enclosures, doors, covers and sheet-metal parts with exposed edges.
2.2.3 Channel and U-Forming Dies
Channel-forming dies are used to create U-shaped, channel-shaped or multi-flange profiles. They can reduce the number of separate bending operations required when compared with forming the same profile using only standard V dies.
Before using channel-forming tooling, verify the required channel width, wall height, material thickness, punch clearance, die geometry and press brake capacity. The completed part must also clear the tooling throughout the bending sequence.
Channel and U-forming dies are suitable for enclosures, structural channels, cabinet parts and profiles with multiple related bends.
2.2.4 Offset and Z-Bend Dies
Offset or Z-bend dies are designed to create two opposing bends and form a stepped profile. They are used when a part requires a controlled offset, return flange or parallel step.
The tooling geometry must match the required offset height, material thickness, bend radius and available tonnage. Offset tooling should not be selected based on profile shape alone; the full part geometry and bending sequence must be checked before production.
Typical applications include stepped panels, mounting brackets, return flanges and sheet-metal parts with parallel offset features.
2.2.5 Radius and Specialty Dies
Radius dies are used when the part requires a smooth curved bend rather than a sharp crease. The final formed radius depends on the material, punch radius, die geometry, bending method and press brake setup.
Other specialty dies may be used for corrugating, non-marking forming, special profiles, large-radius bends and custom sheet-metal applications. For non-standard tooling, provide the part drawing, material thickness, bend angle, inside radius and required finished profile before selecting a tooling solution.
For a detailed guide to die designs, applications and selection, see our Press Brake Dies: Types and Selection Guide.
3. Complete Press Brake Tooling System
A complete press brake tooling system includes all components required to hold, align, and apply forming force accurately during bending. In most production setups, the system includes the following parts:
3.1 Upper punch
The punch is the upper forming tool. Its tip angle, radius, height, and profile determine the bend shape, minimum flange length, and part clearance.
3.2 Lower die
The die supports the sheet metal from below. Its V-opening controls bending tonnage, inside radius, and material deformation.
3.3 Tool holder
The tool holder connects the punch or die to the machine beam. A worn or incompatible holder can cause misalignment, angle inconsistency, and premature tool wear.
3.4 Clamping system
The clamping system locks the tooling into position. Manual clamping is suitable for low-changeover production, while hydraulic or mechanical quick clamping is better for frequent tool changes and automated bending.
3.5 Crowning compensation
Crowning systems compensate for ram and bed deflection during long bends. Without proper crowning, the center and ends of the part may form at different angles.
3.6 Tooling accessories
Common accessories include radius inserts, hemming tools, offset adapters, segmented tool sections, and protective films for mark-free bending.
Understanding the full tooling system is important because bending accuracy depends not only on the punch and die, but also on how the tools are held, aligned, and supported during every stroke.
3.7 How the Tooling System Works Together
A press brake tooling system works as a coordinated set rather than as individual components. The upper punch is mounted to the upper tool holder or clamping system, while the lower die is secured to the lower holder. During bending, the punch applies force to the sheet against the die opening. Depending on the machine and application, crowning or compensation systems help maintain consistent bending results across the working length. Tooling accessories and adapters can be added when special geometries or machine configurations require them.
| Component | Main Function |
|---|---|
| Punzón superior | Forms the inside of the bend |
| Lower die | Supports the sheet and determines the V-opening |
| Tool holder | Secures the punch or die to the machine |
| Clamping system | Holds and allows tooling to be changed |
| Crowning system | Compensates for machine/table deflection |
| Accessories | Support special bending applications |
4. How to Select Press Brake Tooling
Selecting the wrong tooling can contribute to angle inconsistency, surface damage and excessive springback in sheet metal bending.
Select press brake tooling in this order: first confirm the material and thickness, then check the required bend geometry and flange clearance, verify the press brake capacity and clamping interface, and finally confirm whether the application requires standard, segmented, non-marking or custom tooling.
The following seven factors should be reviewed before selecting a punch, die or complete tooling configuration:
For a more detailed decision-making framework covering material analysis, machine compatibility, tooling materials, coatings, and total cost of ownership, read our guide on Choosing The Right Press Brake Tooling: Your Most Critical Production Decision.
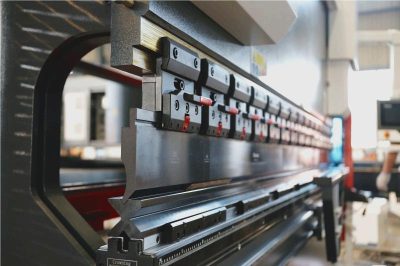
4.1 Material Type
Material type affects the required tooling strength, punch radius, die opening, and risk of surface damage. The ratios below are practical starting points for air bending, not universal rules:
- Acero dulce — a V-opening near 8× sheet thickness is a common starting point for general air bending.
- Acero inoxidable — a wider V-opening may be required because of higher strength and springback; verify the grade, thickness, grain direction, desired inside radius, and available tonnage.
- Aluminio — select the punch radius and die opening according to alloy, temper, surface-finish requirements, and cracking risk; protective film or mark-reducing tooling may be appropriate for visible parts.
Always confirm tooling hardness, load capacity, V-opening, punch radius, and maximum allowable tonnage with the tooling supplier’s data before production.
4.2 Sheet Thickness
Thickness determines the required V-opening size directly. As a general rule, thicker material requires a wider V-opening to reduce tonnage and avoid cracking at the bend line. See Section 6 for the full V-opening reference table.
4.3 Required Bend Angle
- 90° standard bends — straight punch or gooseneck punch
- Acute angles below 60° — dedicated acute angle punch required; standard punches cannot reach the final angle without damaging the die
- Closed hems — hemming punch and flat die; two-stage process
- Large radius bends — radius punch to form a smooth curve without crease marks
4.4 Part Geometry and Flange Length
Box and tray shapes with tall side flanges require a gooseneck punch to avoid the punch body colliding with the already-formed walls during bending. Always check the clearance between the punch profile and the finished part before setup.
4.5 Production Volume and Change Frequency
- High-mix, low-volume — European segmented tooling allows fast reconfiguration for different part lengths
- Long straight bends, high volume — American one-piece tooling offers higher rigidity and lower tooling cost per meter
- Automated or robotic bending cells — WILA/Trumpf precision tooling with hydraulic quick-change clamping can significantly reduce setup time
4.6 Machine Compatibility
Tooling must match the clamping interface of your press brake. European, American, and WILA systems use different tang dimensions and slot geometries and are not interchangeable without adapters. See Section 3 for full compatibility details.
4.7 Tooling Configuration and Clamping Standard
Before selecting press brake tooling, check how the tooling is mounted to the machine. The required configuration may depend on the press brake model, upper and lower tooling arrangement, tooling standard, and clamping system. Confirm these specifications before ordering replacement or additional tooling.
| Compatibility Check | What to Confirm |
|---|---|
| Machine model | Press brake manufacturer and model |
| Upper tooling | Punch type and mounting configuration |
| Lower tooling | Die type and holder configuration |
| Tooling standard | European, American, WILA, Trumpf, etc. |
| Clamping | Manual, hydraulic, pneumatic, or other system |
| Working length | Required tooling length |
5. Press Brake Tooling Standards and Machine Compatibility
Press brake tooling standards determine whether a punch, die, holder and clamping system can be installed safely and accurately on a specific machine. European, American, WILA, Trumpf and other tooling families use different tang profiles, tool heights, loading directions and clamping interfaces.
Before purchasing replacement or additional tooling, verify the press brake model, ram interface, tool profile, holder geometry, loading method, safety features and rated load. Similar-looking tooling systems are not automatically interchangeable.
5.1 European Type Tooling (Euro / Promecam Style)
European / Promecam-style tooling is widely used on CNC press brakes and is commonly available in segmented lengths for flexible setup. However, tang profiles, safety features, loading directions, and clamping interfaces vary by tooling series and manufacturer.
Key characteristics:
- Segmented sections can be combined for different bending lengths.
- Precision-ground options are available for applications requiring consistent tool height.
- Manual, mechanical, and hydraulic clamping options are available, depending on the machine and holder.
- Compatibility must be confirmed from the exact tooling profile and clamping-system specification; similar-looking systems are not automatically interchangeable.
Best for: Job shops, high-mix production, and CNC bending operations that require flexible tooling lengths and frequent changeovers.
5.2 American Type Tooling
American-style tooling is commonly used for robust general-purpose and heavy-duty bending. Depending on the tooling series, it may be supplied in longer sections or segmented sets and may use a self-seating or slot-based mounting profile.
Key characteristics:
- Robust construction for general and heavy-duty bending.
- Long sections can support repetitive straight bends.
- Section lengths, loading method, safety features, and clamping geometry vary by supplier.
- An adapter or compatible holder may be required when using it on a machine designed for another tooling standard.
Best for: Long repetitive bends, heavy-duty work, and shops already standardized on an American-style clamping system.
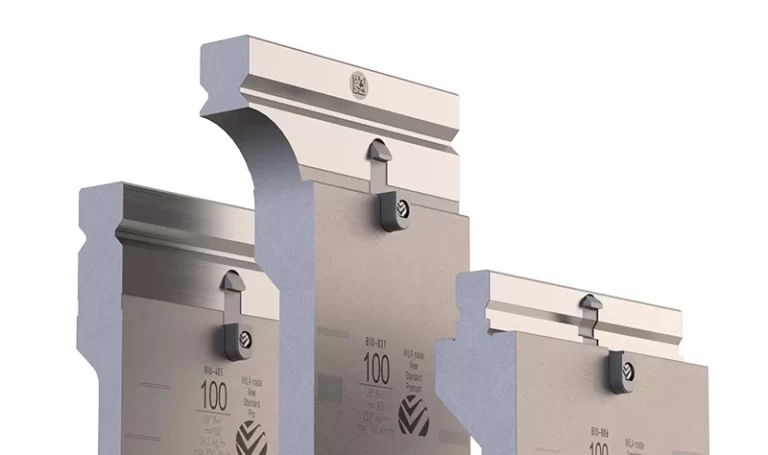
5.3 WILA / Trumpf Precision Tooling
Precision-ground tooling systems, including WILA- and Trumpf-compatible families, are designed for accurate tool alignment, repeatable setup, and efficient changeovers. Their tang profiles, safety mechanisms, sectional lengths, and clamping interfaces vary by series and are not universally interchangeable.
Key characteristics:
- Precision-ground tool height for repeatable setup.
- Mechanical or hydraulic quick-clamping options, depending on the holder.
- Segmented tooling configurations for flexible bending lengths.
- Suitable for CNC and automated bending when the tooling, holder, machine, and robot-loading method are verified as a complete system.
Best for: High-mix production, precision bending, quick-change applications, and automated cells using a verified compatible tooling system.
5.4 European vs American Press Brake Tooling: Quick Comparison
| Factor | European / Promecam Style | American Style |
|---|---|---|
| Typical format | Often supplied in segmented sections | Often supplied in longer sections; segmented options also exist |
| Setup flexibility | Well suited to frequent length changes | Well suited to repetitive setups and long straight bends |
| Clamping | Manual, mechanical, or hydraulic systems are available | Clamping method depends on the machine and tooling series |
| Compatibility | Profile and safety features must match the holder | Profile and safety features must match the holder |
| Before purchasing | Verify tang profile, dimensions, loading direction, safety system, tool height, and load rating | Verify tang profile, dimensions, loading direction, safety system, tool height, and load rating |
5.5 Tool Holders and Clamping Systems
Press brake tool holders and clamping systems secure the punch and die in the correct position during bending. They directly affect tool alignment, setup speed, bending accuracy, and operator safety.
A press brake punch holder connects the upper punch to the ram. Its main function is to keep the punch centered and locked during the bending stroke. If the punch holder is worn, loose, or incompatible with the tooling standard, the punch may shift under load and cause angle inconsistency.
A press brake die holder supports the lower die on the worktable. It keeps the die aligned with the punch centerline and helps maintain consistent contact across the bending length.
Common holder and clamping options include:
Manual clamping — economical and suitable for low-volume production, but slower during frequent tool changes.
Mechanical quick clamping — improves setup speed and repeatability compared with standard manual clamps.
Hydraulic clamping — ideal for CNC press brakes, high-mix production, and automated bending cells because it provides fast, uniform, and repeatable tool locking.
Tool holder compatibility must always match the tooling standard. European, American, and WILA / Trumpf systems use different tang dimensions, slot geometries, and clamping interfaces. Incompatible holders can cause poor alignment, unsafe loading, and inaccurate bends.
Before selecting a tool holder or clamping system, confirm the machine model, ram interface, punch tang size, tool height, loading direction, and required changeover frequency.
6. Press Brake Tooling Materials
Tooling material determines how well the punch and die hold their shape under repeated high-tonnage cycles. The wrong material choice leads to accelerated edge wear, angle drift, and in severe cases, tool cracking during production. The four materials below cover the full range of industrial applications from budget light-duty work to high-precision automated lines.
Common Tooling Materials Compared
| Material Type | Hardness Level | Advantages | Typical Use Cases |
|---|---|---|---|
| 42CrMo Alloy Steel | Medium–High | High strength, good durability, cost-effective | Standard punches/dies for mild steel & stainless steel |
| T8 / T10 Carbon Steel | Medium | Simple forming jobs, easy to machine | Budget tooling, light production |
| H13 Tool Steel (Heat-treated) | High | Excellent hardness, heat resistance, long service life | Heavy-duty bending, high tonnage jobs |
| Carbide Tipped Tools | Very High | High wear resistance and consistent performance in suitable high-cycle applications | High precision bending, thin stainless steel, mass production |
Practical selection guidance:
Tooling material should be selected according to the workpiece material, required tonnage, production volume, target accuracy, surface-finish requirements, and the tooling supplier’s heat-treatment specification. Alloy tool steels are commonly used for general production, while higher-wear-resistance grades or specialized inserts may be appropriate for demanding or high-cycle applications. Do not select a tooling grade from material name alone; verify hardness, toughness, allowable load, heat treatment, and regrinding requirements with the tooling manufacturer.
Steel vs Urethane Press Brake Tooling
Steel and urethane press brake tooling are used for different bending requirements. Steel tooling is the standard choice for most industrial bending jobs, while urethane tooling is mainly used when surface protection is more important than maximum forming force.
Steel tooling is best for general sheet metal bending, high-tonnage applications, tight angle control, and long tool life. It provides excellent rigidity and repeatability, making it suitable for mild steel, stainless steel, and heavy-duty production.
Urethane tooling is used for mark-free bending, especially on polished aluminum, painted sheets, pre-coated panels, and decorative surfaces. Instead of forming the sheet directly against a hard steel die edge, urethane tooling supports the material with a softer contact surface to reduce scratches, dents, and surface marks.
Urethane tooling is generally used for lower-load, surface-sensitive applications. Its allowable load, deformation behavior, and service life depend on urethane grade, geometry, material thickness, and production conditions.
Comparison:
| Tooling Type | Best For | Advantages | Limitations |
|---|---|---|---|
| Steel tooling | Standard bending, high tonnage, precision work | High strength, long life, accurate bends | May leave marks on soft or coated materials |
| Urethane tooling | Mark-free bending, coated sheets, polished materials | Reduces scratches and surface damage | Lower load capacity, wears faster, less suitable for heavy forming |
For most production environments, steel tooling should remain the primary choice. Urethane tooling is best used as a surface-protection solution when part appearance is critical.
7. Press Brake V-Opening Selection Guide
The V-opening is one of the most important die parameters in air bending because it influences required tonnage, the resulting inside radius, minimum flange length, and the risk of cracking or surface damage. It controls three things simultaneously: the tonnage required to complete the bend, the inside bend radius formed on the part, and the risk of cracking at the bend line.
The standard selection rule is:
A common starting point for air bending mild steel is: V-opening ≈ 8 × sheet thickness. This is a preliminary selection rule, not a substitute for the tooling supplier’s capacity chart or a verified bending calculation.
However, this ratio changes with material type. Stainless steel has higher tensile strength and work-hardens faster, requiring a wider opening to reduce cracking risk. Aluminum is softer but more prone to surface marking on the die contact edges, so a wider opening reduces the contact pressure.
Common starting ranges for air bending:
- Mild steel / cold-rolled steel: begin near
V = 8 × t, then verify tonnage, radius, and minimum flange length. - Stainless steel: a wider opening may be required depending on grade, strength, springback, and grain direction.
- Aluminum: select the opening according to alloy, temper, desired radius, surface requirements, and cracking risk.
How to Choose the Right V-Opening
The correct V-opening depends primarily on material type, sheet thickness, bending method, and the required inside bend radius. For air bending, a wider V-opening generally reduces the required bending force but increases the inside bend radius, while a narrower opening increases forming force and may affect the workpiece or tooling.
As a starting point, fabricators commonly select the V-opening based on sheet thickness and material, then adjust it according to the required bend radius, machine capacity, and tooling limitations.
Example Starting V-Openings for Air Bending
The following values are preliminary examples for planning only. Final die selection must be checked against the tooling supplier’s chart, press capacity, material certificate, target radius, and minimum flange requirement.
| Sheet Thickness (mm) | Mild Steel V (mm) | Stainless Steel V (mm) | Aluminum V (mm) | Notes |
|---|---|---|---|---|
| 0.5–1.0 | 6–8 | 8–10 | 10–12 | Precision bending, thin gauge |
| 1.5–2.0 | 12–16 | 16–20 | 20–24 | General fabrication |
| 3.0–4.0 | 24–32 | 32–40 | 36–48 | Reduces tonnage requirement |
| 6.0–8.0 | 48–64 | 60–80 | 72–96 | Heavy-duty applications |
Critical limits:
V too small — the sheet metal cannot deform smoothly into the die. Stress concentrates at the bend line, causing cracking or fracture on the outer surface. A V-opening below 6× sheet thickness generally increases tonnage and cracking risk. Always verify the tooling supplier’s capacity chart, material properties, bend radius, and press brake tonnage before using a narrower opening.
V too large — the punch travels too deep relative to the die contact points before the sheet reaches the target angle. This reduces angle accuracy and increases springback, making it difficult to hold tight angle tolerances.
Inside bend radius relationship: When air bending, the inside bend radius formed on the part is approximately 1/6 of the V-opening width. For example, a 24 mm V-die produces approximately a 4 mm inside radius on mild steel. If a specific inside radius is required by the part drawing, work backward from this relationship to select the correct die.
8. Tooling Maintenance & Longevity
Tooling failure rarely happens suddenly. In most cases, it is the result of accumulated neglect — contaminated contact surfaces, improper storage, or misalignment that has been ignored for weeks. A structured maintenance routine requires little time, can help extend tooling service life, and can reduce angle drift and surface defects caused by contamination, damage, or uneven wear.
8.1 Pre-Shift Cleaning & Surface Care
Frequency: Before every production shift
Before loading any tooling, wipe down punch tips and die grooves with a clean cloth to remove metal chips, dust, and oxide buildup from the previous shift. Even small particles trapped between the tool and the sheet will cause surface marks on the part and create uneven contact that throws off bend angles.
Use only non-corrosive cleaning solutions approved for tool steel. Avoid abrasive cloths or wire brushes on ground tool surfaces — they introduce micro-scratches that accelerate wear. Pay particular attention to the V-groove of the die, where chips tend to accumulate at the bottom and are easy to overlook.
8.2 Controlled Lubrication
Frequency: As needed based on material and production volume
Apply a thin film of light machine oil to punch tips and die contact edges to reduce friction during bending. This is especially important when bending stainless steel, which has a tendency to gall against tool steel surfaces under high contact pressure.
Do not over-lubricate. Excess oil migrates onto the sheet metal surface, causing contamination that interferes with downstream welding, coating, or painting operations. On WILA-style hydraulic clamping systems, never apply oil to the clamping mechanism itself unless the manufacturer's documentation specifically permits it — hydraulic clamps are sealed systems and external lubrication can damage the seals.
8.3 Safe Handling & Storage
Frequency: Every time tooling is removed from the machine
Press brake tooling is precision-ground to tight tolerances. A single drop onto a concrete floor can introduce micro-cracks that are invisible to the naked eye but cause angle inconsistency and eventually lead to tool fracture under load.
Store punches and dies in dedicated tooling racks or padded protective cases. Organize tools by type, height, and V-opening size — clearly labeled — so operators can locate the correct tool without handling multiple pieces unnecessarily. Keep storage racks close to the machine to minimize the distance tools are carried by hand.
Never stack dies directly on top of each other without protective separators. The V-groove edges are the most vulnerable part of the die and are easily chipped by contact with other hard surfaces.
8.4 Alignment & Crowning Verification
Frequency: At the start of each new job setup
Misaligned tooling creates torsional stress on both the punch and die, causing uneven wear across the tool length and inconsistent angles from one end of the bend to the other. Before starting production, verify that the punch centerline sits directly over the die V-groove centerline across the full working length.
For bending lengths over 1,000 mm, check the crowning system setting. Press brake beams deflect under load — the crowning system compensates by applying additional force at the center of the beam. If the crowning value is not correctly set for the current tonnage and tooling length, the center of the part will bend to a different angle than the ends. Check and adjust crowning whenever material thickness or bend length changes significantly.
Replace damaged tool holders immediately. A worn or cracked holder allows the punch to shift laterally during the stroke, which accelerates tool wear and makes accurate bending impossible.
8.5 Edge Sharpening & Life Restoration
Frequency: When angle deviation appears that cannot be corrected by machine adjustment
Some press brake tooling — particularly carbon steel and certain alloy steel tools — can be reground to restore the punch tip or die edge geometry after wear. This is a cost-effective alternative to full tool replacement when the rest of the tool body is still in good condition.
However, regrinding reduces tool height. Because press brake controllers reference the tool height for stroke depth calculations, any height change after regrinding must be measured accurately and updated in the machine controller settings. Failure to do this results in incorrect bend angles immediately after the tool returns to service.
Do not regrind carbide-tipped tools — the carbide layer cannot be restored by conventional grinding and attempting to do so damages the substrate. Replace carbide tools when worn.
After any regrinding operation, measure tool height at multiple points along the length with a micrometer and confirm uniformity before returning the tool to production.
9. Common Tooling Defects & Troubleshooting
Most press brake tooling problems fall into a small number of repeatable patterns. The table below covers the most common defects, their root causes, and corrective actions. When a defect appears, always rule out material variation and machine calibration issues before replacing tooling — in many cases the tool itself is not the primary cause.
| Defect | Possible Causes | Checks and Corrective Actions |
|---|---|---|
| Cracking during bending | V-opening too narrow; punch radius too small; low material ductility; unfavorable grain direction | Verify material grade and grain direction; review punch radius and V-opening; confirm tonnage and minimum flange limits |
| Angle inconsistency | Tool wear; incorrect crowning; holder misalignment; material-thickness variation | Inspect and align tooling; verify holder condition and crowning; measure material thickness along the bend |
| Surface marks | Contaminated tooling; sharp contact edges; unsuitable contact pressure; sensitive coated surface | Clean and inspect tooling; consider protective film, polished radii, or suitable mark-reducing tooling |
| Excessive springback | Material strength variation; unsuitable bend method; incorrect stroke or tool geometry | Verify material data; review stroke depth, punch radius, die opening, and bending method; perform a controlled test bend |
Need standard or custom tooling for a specific press brake? Explore our Utillaje para prensas plegadoras solutions for punches, V-dies, segmented tooling, hemming tooling and custom forming requirements.
10. Conclusion
Press brake tooling selection is not a one-size-fits-all decision. The right combination of punch type, die geometry, V-opening width, and tooling material depends on your specific material, part geometry, and production requirements. Getting these parameters right from the start eliminates the most common sources of bending defects — angle inconsistency, surface marking, and cracking — before they reach production.
Selecting the right press brake tooling requires more than matching a punch and die. Material, thickness, bend geometry, V-opening, tooling standard, clamping configuration, and machine compatibility all affect the final tooling choice.
For tooling recommendations, provide your press brake model, tooling standard, material grade, sheet thickness, bend length, and part drawings so the appropriate tooling configuration can be evaluated.
11. FAQ
For 3 mm stainless steel, a V-opening around 30–40 mm may be used as a starting range for air bending, depending on the material grade, required bend radius, tooling configuration, and machine capacity.
Not directly in most cases. European / Promecam and American-style tooling families use different mounting and clamping geometries. A compatible adapter or replacement holder may be required. Before installation, verify the exact tang profile, tool height, loading direction, safety mechanism, holder geometry, and rated load with the machine and tooling suppliers.
Air bending, bottoming, and coining are three distinct forming methods. In air bending, the sheet contacts the punch tip and die shoulders without fully conforming to the die cavity; the final angle is mainly controlled by stroke depth. In bottoming, the sheet is pressed more closely against the die surfaces, so the punch and die angles must suit the target bend and expected springback. Coining uses much higher pressure to plastically compress the bend area and is not simply another name for bottoming. Tooling geometry, allowable load, and machine tonnage must be verified separately for each method.
There is no fixed interval. Inspection or reconditioning should be based on measurable wear, edge damage, tool-height variation, angle drift, surface defects, material type, and production volume. After regrinding, measure the tool height along its full length and update the machine’s tooling data. Coated, carbide-tipped, or specialized tooling should only be reconditioned according to the manufacturer’s instructions.
The three most common causes are: (1) incorrect crowning — the press brake beam deflects under load, and if the crowning compensation is not set correctly for the current tonnage and bend length, the center of the part bends to a different angle than the ends; (2) non-uniform tool height — if segments in a segmented tooling set have worn to different heights, contact is uneven along the bend line; (3) material thickness variation — if the incoming sheet has thickness variation beyond the material specification, the bend angle will vary correspondingly. Check crowning settings first, then measure tool height uniformity along the full working length, and finally verify material thickness at multiple points on the sheet.
The rule of 8 is a common starting point for air bending mild steel: the V-die opening is selected at approximately eight times the sheet thickness. It is not a universal rule. Final selection should also consider material grade and tensile strength, grain direction, target inside radius, minimum flange length, available tonnage, punch radius, and the tooling supplier’s capacity chart.
Quiénes somos
Durmapress se especializa en el diseño, la fabricación y la venta de diversos equipos de procesamiento de metales, como plegadoras, cizallas, punzonadoras, máquinas de corte por láser, etc. La empresa se fundó en 2000. Con años de experiencia y acumulación de tecnología. DurmaPress se ha convertido en una de las marcas más conocidas de la industria china de maquinaria para el procesamiento de metales.
Contáctenos
Entradas recientes
Categorías
Síganos
Nuevo vídeo semanal
Más información
Si tiene alguna información sobre nuestros productos, póngase en contacto con nosotros y le responderemos en 24 horas.