Punching Force Formula: Quick Answer
How to Calculate Punching Force
Use the basic formula first:
F = L × t × τ
For a circular hole:
L = π × d
Where:
- d = hole diameter, in mm
- L = hole perimeter, in mm
- t = sheet thickness, in mm
- τ = material shear strength, in MPa or N/mm²
- F = punching force, in N
If only tensile strength is available, use a verified material-data source or a conservative engineering assumption to estimate shear strength. Do not treat tensile strength and shear strength as identical material properties.
For press selection, apply a safety factor after calculating the basic force:
Required press force = Basic punching force × safety factor
The suitable safety factor depends on die condition, clearance, material variation, lubrication, process stability, and the press manufacturer’s operating limits.
What Is Punching Force?
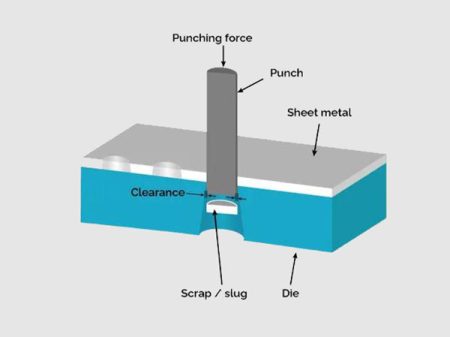
Punching force, also called blanking force, is the force required for a punch and die to shear through sheet metal and create a hole, slot, or blanked profile.
The required force depends mainly on material shear strength, sheet thickness, and total cut perimeter. In general, stronger material, thicker sheet, and a longer cut perimeter all require higher punching force.
Why Punching Force Matters for Press Tonnage Selection
Punching-force calculation helps determine whether a punch press, tool set, and die design can complete an operation safely and repeatedly.
Use the calculated force to check:
- Whether the press has sufficient rated tonnage;
- Whether the required tonnage is available at the operating point;
- Whether the punch and die can withstand the load;
- Whether tool wear or material variation could exceed available capacity;
- Whether a different tool design, clearance, or process is required.
Learn how machine capacity, tooling, applications, and process requirements affect equipment selection in this hydraulic punch press guide.
How to Calculate Punching Force
Use the basic punching-force formula:
F = L × t × τ
Where:
- F = punching force, in N
- L = total cut perimeter, in mm
- t = material thickness, in mm
- τ = material shear strength, in MPa or N/mm²
For a circular hole, calculate the cut perimeter first:
L = π × d
Where d is the hole diameter in mm.
For machine selection, calculate the basic force first. Then apply a suitable safety factor based on die condition, punch and die clearance, lubrication, material variation, and the press manufacturer’s operating limits.
Punching Force Calculation Example: Round Hole in Mild Steel
Assume you need to punch a 20 mm diameter hole in 3 mm mild steel.
- Hole diameter: d = 20 mm
- Material thickness: t = 3 mm
- Material shear strength: τ = 300 MPa
Step 1: Calculate the hole perimeter
L = π × d
L = 3.1416 × 20
L = 62.83 mm
Step 2: Calculate the basic punching force
F = L × t × τ
F = 62.83 × 3 × 300
F = 56,547 N
Step 3: Convert force to metric tons
Press tonnage = 56,547 ÷ 9,807
Press tonnage = 5.77 metric tons
This is the theoretical punching force. Final press selection must also consider the safety margin, die clearance, tooling condition, material tolerance, and available machine capacity.
Sheet metal punching
Punching Force Calculator
Estimate the theoretical punching force and press tonnage from cut perimeter, sheet thickness, and material shear strength.
F = L × t × τ
Calculated result
- Cut perimeter
- —
- Basic punching force
- —
- Basic punching force
- —
- Theoretical press tonnage
- —
This is an engineering estimate, not a machine-selection guarantee. Confirm press rating at the operating point, tooling condition, die clearance, material variation, and manufacturer limits before production.
What Affects Actual Punching Force?
Material shear strength
Higher-strength material requires more punching force. Use material-specific shear-strength data whenever possible.
Sheet thickness
Punching force increases directly as sheet thickness increases.
Cut perimeter
A larger hole, longer slot, or more complex profile increases the total cut perimeter and therefore increases required force.
Die clearance and tool condition
Incorrect clearance, worn punch edges, or poor alignment can increase force demand and shorten tool life.
Lubrication and material condition
Surface coatings, work hardening, burrs, and inconsistent material condition can affect punching performance and required force.
How Punching-Force Calculations Are Used
Punching-force calculations are used to:
- Select a press with sufficient working tonnage;
- Size punches, dies, and tool components;
- Check whether a hole or blanking operation is practical;
- Reduce the risk of punch breakage, excessive burrs, and poor edge quality;
- Compare tooling and process options before production.
For sheet-metal hole punching and forming applications, explore DurmaPress hydraulic punching machines.
Sobre nós
A Durmapress é especializada na conceção, fabrico e venda de vários equipamentos de processamento de metal, incluindo máquinas de dobragem, tesouras, punções, máquinas de corte a laser, etc. A empresa foi fundada em 2000. Com anos de experiência e acumulação de tecnologia. DurmaPress tornou-se uma das marcas bem conhecidas na indústria de máquinas de processamento de metal da China.
Contate-nos
Categorias
Siga-nos
Novo vídeo semanal
Contacte-nos para mais informações
Se tiver alguma informação sobre os nossos produtos, contacte-nos e responderemos no prazo de 24 horas.